CNC Router Cutting Aluminium Guide: Tooling, Speeds, Workholding, and Finish Quality
Ask ten hobbyists whether a router can cut aluminium and you will get ten different answers, most of them wrong in one direction or the other. Some insist it is impossible on anything but a mill; others promise it is trivial and then post pictures of a bit welded solid with melted metal. The truth sits in the middle. Cutting aluminium on a CNC router is absolutely possible, but it is a process where each step depends on the others, and skipping one is what turns a clean cut into a ruined bit.
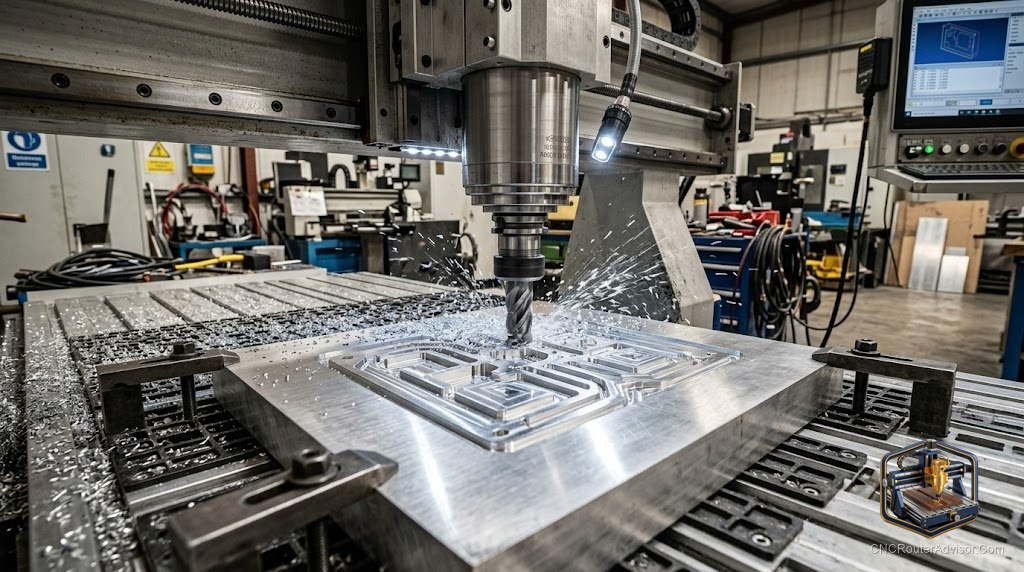
Cutting aluminium on a CNC router means machining aluminium sheet, plate, or extrusion on a router by combining a rigid setup, the right tooling, correct feeds and speeds, solid workholding, and cooling with chip clearing. The single biggest cause of failure is chips welding to the tool from heat and poor evacuation, so the whole approach is built around cutting real chips and getting them out fast.
Short answer: to cut aluminium on a router, use a rigid machine, a single-flute carbide end mill, shallow passes at the correct chip load, a lubricant or coolant, aggressive chip clearing, and rock-solid workholding. Run a feed high enough to make chips rather than dust, and never let the bit dwell and rub. Get one of these wrong and you get gumming, chatter, or a broken tool.
Why aluminium is different
Aluminium is soft, but it is sticky when it heats up. Unlike wood, which produces chips that fall away, aluminium chips can weld themselves to a hot bit, clogging the flutes and causing the tool to smear rather than cut. Manage heat and chips and aluminium cuts cleanly; let heat build and the cut fails fast. Every technique below serves those two goals.
Machine setup
Start with rigidity. Aluminium cutting forces are much higher than wood, and flex causes chatter and broken tools. You want:
- A stiff frame, steel or heavy aluminium, that resists deflection.
- Ball or lead screws and linear rails for backlash-free motion.
- A spindle with real torque, such as a water-cooled VFD spindle from around 700W upward.
- A flat, solid bed for secure holding.
Tooling
- Single-flute end mills are the go-to for aluminium. The single flute leaves maximum room for chips to clear before they weld to the tool.
- Two-flute end mills give a finer finish once you have feeds dialed in.
- Carbide, not high-speed steel, since carbide holds its edge in metal.
- Sharp only. A dull tool rubs, heats, and breaks.
Feeds and speeds
The target is a proper chip load, chips thick enough that they carry heat away with them. That means:
- Shallow depth of cut with multiple passes.
- Moderate RPM, not the router’s maximum, matched to the tool.
- A feed rate that keeps the bit shearing chips, never dwelling.
Watch and listen: small bright chips and a steady shearing sound are right; a high squeal or fine powder means the bit is rubbing and heating.
Cooling and chip clearing
Heat control is non-negotiable in aluminium:
- Cutting fluid or mist coolant cools the tool and lubricates the cut.
- A light lubricant like WD-40 helps on lighter setups.
- A cold air gun cools and blows chips clear.
- Constant chip evacuation keeps chips from re-cutting and welding.
Workholding
Aluminium will not tolerate a part that moves. Use a solid vise, strong clamps, or a bolted fixture so the workpiece cannot shift or vibrate. Movement means chatter, ruined finish, and snapped bits.
Finish quality and troubleshooting
A good aluminium finish is bright and smooth. Fix problems by their cause:
- Gummed, welded bit: poor chip clearing and heat; use a single-flute bit, add cooling, clear chips, raise feed relative to RPM.
- Chatter marks: improve rigidity, reduce depth, check workholding, adjust feeds.
- Smeared or torn surface: the bit is rubbing; increase chip load or replace a dull tool.
- Broken tools: reduce depth per pass, slow the plunge, confirm workholding.
Product picks
FoxAlien XE-PRO (rigid entry for light aluminium). A stout, affordable machine that handles light aluminium with careful technique, a practical way to learn metal cutting without a mill. Honest flaw: it is still a light machine, so keep passes shallow and feeds patient; it will not remove metal quickly. On Amazon.
SpeTool single-flute end mills (aluminium tooling). Single-flute carbide bits built to clear chips in aluminium, the correct starting tooling for clean metal cuts. Honest flaw: single-flute geometry leaves a slightly coarser finish, so a two-flute bit is better for finishing passes. On Amazon.
The bottom line
Cutting aluminium on a CNC router is a system where rigidity, single-flute carbide tooling, correct feeds and speeds, solid workholding, and cooling with chip clearing all work together. The enemy is heat and welded chips, so run real chip loads, keep the cut cool, and clear chips relentlessly. Start shallow, listen to the cut, and build up as you learn the machine. Do it right and a router turns out bright, clean aluminium parts.
FAQ
Can a CNC router cut aluminium? Yes, with a rigid machine and the right tooling, feeds, workholding, and cooling. The key is managing heat and clearing chips so they do not weld to the bit.
Why does my bit gum up in aluminium? Chips are welding to a hot tool. Use a single-flute bit, add cooling, clear chips constantly, and raise feed relative to RPM.
What bit is best for aluminium? A single-flute carbide end mill, which gives chips maximum room to clear. Use a two-flute bit for finer finishing passes.
Do I need coolant for aluminium? Some cooling is important. Cutting fluid, mist coolant, a light lubricant like WD-40, or a cold air gun all reduce heat and improve the cut.
How deep can I cut aluminium? Shallow passes only, building depth over several passes. Deep single passes cause chatter, welding, and broken tools.
What feeds and speeds work for aluminium? Moderate RPM with a feed high enough to make real chips that carry heat away. Slow feeds at high RPM cause rubbing and welding.
How do I get a clean finish on aluminium? A rigid setup, sharp single-flute tooling, correct chip load, cooling, solid workholding, and a lighter finishing pass with a two-flute bit.
References
- CNCRouterInfo, how to choose a CNC router: https://cncrouterinfo.com/guides/how-to-choose-a-cnc-router/
- CNC Dad, best CNC router for beginners: https://www.cnc-dad.com/blog/best-cnc-router-for-beginners/